Screening Gear Micropitting Through Oil Temperature DOE
Micropitting is a fine-scale fatigue mechanism that can begin quietly on highly loaded gear teeth before it becomes visible as conventional pitting, scuffing, or destructive surface damage. In an aircraft reduction gearbox, small changes in lubricant temperature can alter viscosity, film thickness, chemical reactivity, heat removal, and the way manufacturing variation appears under load. A structured design-of-experiments study helps separate those effects from the influence of speed, torque, surface finish, and alignment.
For geared aircraft engines, this question has practical importance. The gearbox must transmit high power in a compact envelope while maintaining low mass, high power density, and predictable service life. The OPTIMIZE initiative examines this broader engineering problem through modelling, tolerance analysis, physical validation, and efficient design methods. Its OPTIMIZE Project resources provide useful context for connecting gear-surface research with complete propulsion-system performance.
Why Micropitting Deserves Early Attention
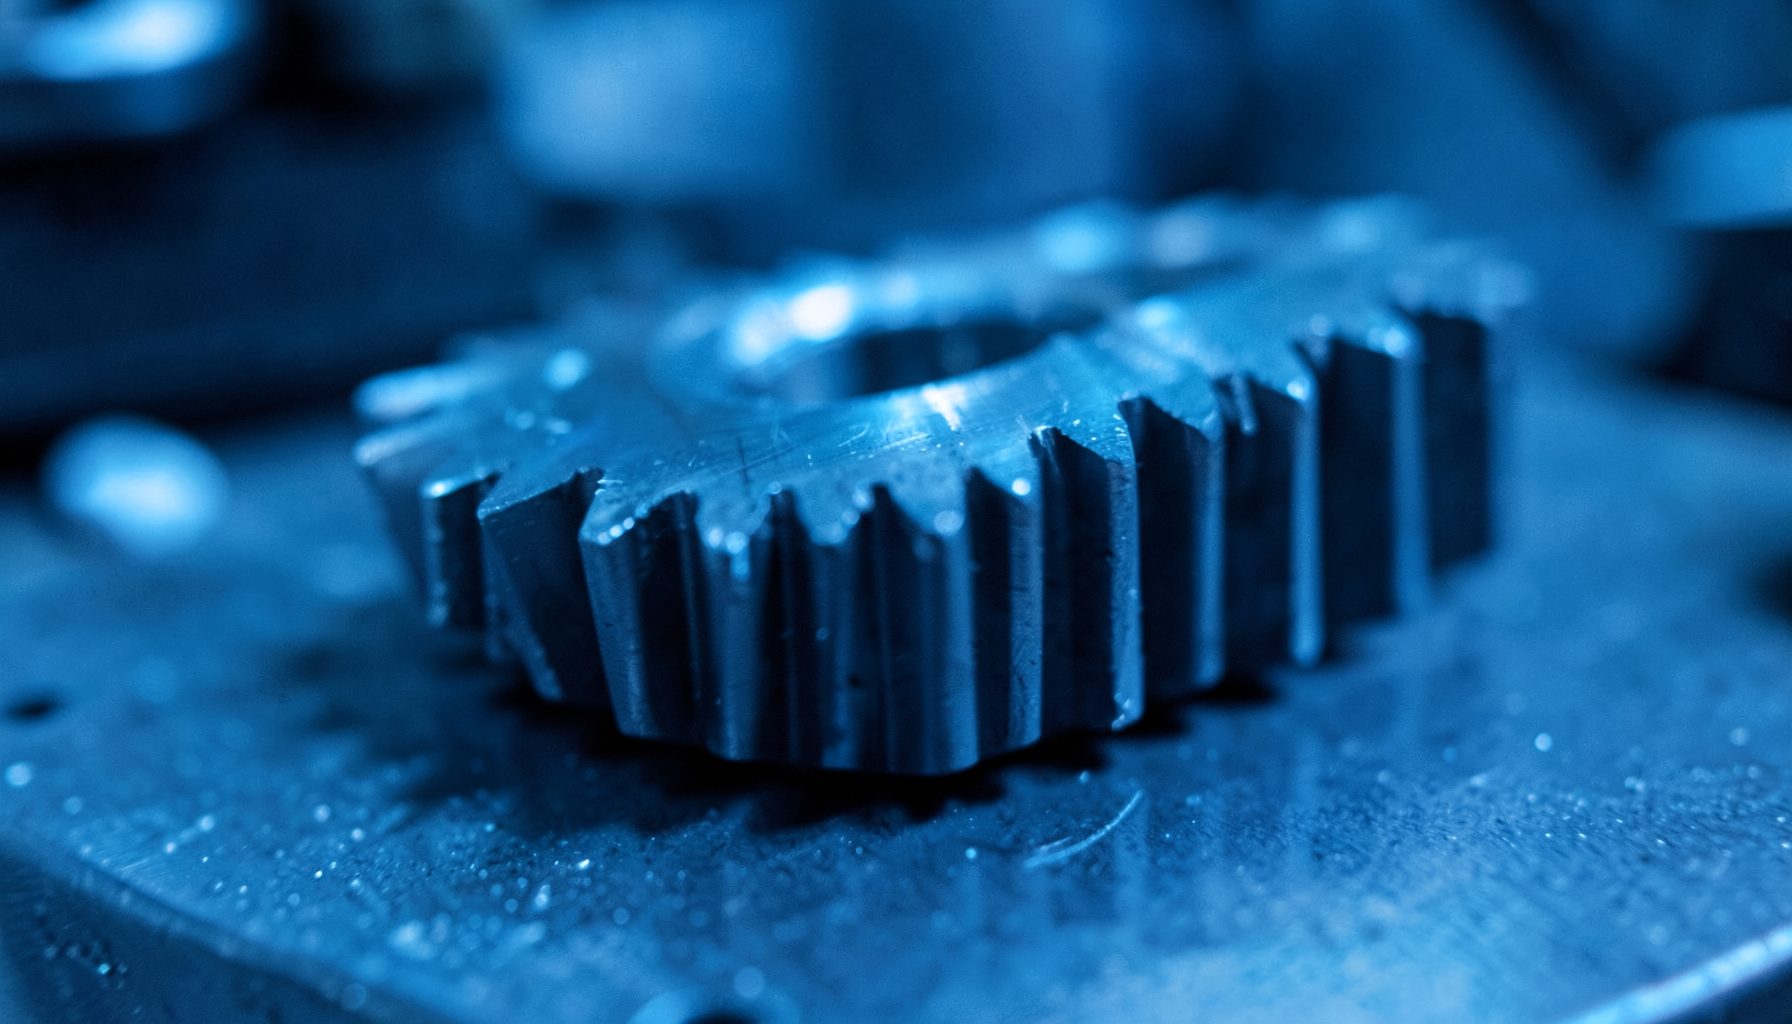
Micropitting consists of small surface fatigue cracks and grey-stained areas that develop in the loaded zone of a gear flank. The damage is associated with repeated asperity interaction, local stress concentration, and an oil film that is too thin to keep opposing surfaces fully separated. At first, the marks may appear cosmetic. Over time, however, they can change the tooth profile, increase sliding losses, generate debris, and create conditions for more severe pitting.
Oil temperature is a strong candidate factor because it changes the lubricant’s rheology. As temperature rises, dynamic viscosity generally falls, reducing elastohydrodynamic film thickness. The same temperature increase may improve flow through the contact and help remove heat, so the response is not necessarily a simple linear deterioration. A cooler oil can provide a thicker film, yet excessive viscosity may increase churning losses and delay delivery to critical regions.
A screening study should therefore measure micropitting initiation rather than assume that the hottest condition is automatically the worst. Initiation can depend on local flash temperature, transient load, surface roughness, additive performance, and the duration of exposure. A design that looks safe at a steady bulk temperature may experience a different risk profile during acceleration, idling, or a brief loss of cooling capacity.
Framing The Experimental Question
The central question can be expressed as: which controllable factors and interactions most strongly affect the first measurable evidence of micropitting, and how does oil temperature modify that response? The response variable might be a binary initiation result, a rating based on affected area, a grey-staining index, or a quantified change in surface texture. Using several responses gives the study more diagnostic value than relying on a single pass-fail outcome.
Oil temperature should be defined carefully. A thermocouple in the sump records bulk temperature, while the gear mesh may experience a substantially different local temperature. The test plan should record inlet temperature, outlet temperature, flow rate, ambient conditions, and, where possible, an estimate of gear-mesh or flash temperature. For Australian test facilities, that distinction matters when a rig operates in a warm Adelaide workshop or under summer conditions in Brisbane, where room temperature can influence cooling performance.
The study should also specify the initiation threshold before testing begins. For example, researchers may define initiation by a prescribed percentage of grey-stained area, a surface profile change beyond measurement uncertainty, or a repeatable microscopy signature. Pre-registering the rule limits subjective decisions after the results are known and makes comparisons between laboratories more credible.
Selecting Factors For A Screening Design
A practical first design may include oil temperature, rotational speed, transmitted torque, oil flow, surface roughness, and gear flank treatment. Temperature could be tested at three levels covering the intended operating window rather than using arbitrary values. Speed and torque should represent realistic combinations, since the contact’s slide-to-roll ratio and generated heat depend on both.
Lubricant condition deserves separate attention. Oil type, additive package, viscosity grade, contamination level, and oxidation state can all influence micropitting resistance. If the project’s immediate objective is temperature sensitivity, the oil formulation should remain fixed while temperature is varied. A later study can then introduce lubricant chemistry as a second-stage factor once the important mechanical effects are known.
Manufacturing variation is especially relevant to aerospace gears. Tooth flank lead, profile error, waviness, roughness, hardness, residual stress, and coating thickness may shift the local contact conditions. A screening design can include representative high and low values for the most influential tolerances, or it can use several physical gear sets to estimate batch-to-batch variation. This links the laboratory result with the tolerance-analysis methods used in the OPTIMIZE work.
For a rig intended to support multiple projects, consistent documentation is essential. Researchers should record sensor calibration, gear identification, oil batch, run-in history, assembly procedure, and test interruptions. A clear setup guide can help standardise practical steps, provided it is adapted to the rig’s actual safety, instrumentation, and cleanliness requirements.
Managing Temperature In The Test Rig
Temperature control must distinguish between setting a target and maintaining a stable contact condition. A circulating oil system may reach the desired inlet temperature while the gear mesh continues to warm during the run. The protocol should define stabilisation time, allowable fluctuation, ramp rate, and whether the temperature is controlled before or during torque application.
Thermal gradients can create misleading results. Oil entering at a fixed temperature may leave hotter after passing through a heavily loaded mesh. Bearings, seals, shafts, and housing walls also contribute heat. Sensors should be placed where they reveal the thermal state of the lubricant and the hardware, rather than relying on one convenient measurement point.
The Australian environment provides useful stress cases for planning. A facility near Darwin may face high ambient temperatures and humidity, while a winter test in Melbourne can start with a very different thermal baseline. These conditions should not replace controlled laboratory levels, but they can inform the range of cooling loads and warm-up times used in the test matrix. Metric units and degrees Celsius should be used consistently in reports and control software.
Lubricant sampling at planned intervals can reveal oxidation, viscosity change, additive depletion, and particle generation. If oil temperature is the treatment factor, chemical changes caused by long high-temperature exposure must be tracked rather than mistaken for a purely thermal effect. This is particularly important when each test run lasts long enough for the oil’s condition to evolve.
Combining Simulation And Physical Evidence
A numerical model can help identify likely high-risk conditions before the full experiment begins. Thermal network models estimate oil and housing temperatures, while contact models evaluate load distribution, sliding, film thickness, and local pressure. Computational results should guide factor ranges and sensor placement, not serve as a substitute for measured initiation data.
The most useful model outputs are often comparative. A model may show that a moderate increase in temperature causes a substantial reduction in minimum film thickness at a particular speed and torque combination. That prediction can then be tested through surface inspection, roughness measurement, and lubricant analysis. Agreement in trends is valuable even when absolute film-thickness predictions contain uncertainty.
Bearing behaviour should be considered because it affects shaft alignment, preload, and oil delivery. Work on bearing shield design illustrates why oil retention and component response must be considered in demanding acceleration environments. In a gearbox study, a change in bearing condition can modify gear contact enough to obscure the temperature effect being investigated.
Inspection should combine visual grading with quantitative methods. Optical microscopy, replica techniques, profilometry, white-light interferometry, and three-dimensional surface scans can detect early changes that are difficult to classify by eye. Repeating measurements on the same tooth locations before and after testing strengthens the evidence for initiation and reduces the influence of initial surface variation.
Analysing Interactions And Uncertainty
A screening DOE is intended to rank effects efficiently, so the statistical model should match the response. For a binary initiation result, logistic regression or a generalised linear model may be appropriate. For a continuous damage index, analysis of variance and response-surface methods can identify main effects, curvature, and interactions. Replicated centre points help reveal non-linearity and provide an estimate of repeatability.
Temperature may interact with speed and torque in ways that are more important than its isolated main effect. At low speed, a temperature increase might mainly reduce viscosity. At high speed, the same increase may coincide with greater churning, stronger heat generation, and a larger drop in film thickness. A temperature-by-load interaction can therefore indicate that a gearbox is robust during cruise but vulnerable during high-power climb or transient operation.
Uncertainty should include measurement error, gear-to-gear variation, sensor drift, oil-property variation, and differences in assembly. Randomising the run order reduces the risk that time-dependent oil degradation or rig wear is confused with a factor effect. Blocking by gear set, test day, or oil batch can preserve useful comparisons when all nuisance variables cannot be held constant.
Data management is part of the engineering method. Raw temperature traces, torque histories, inspection images, and analysis scripts should remain linked to the run identifier. Teams preparing a public project page can consult practical hosting guidance while ensuring that sensitive aerospace information, proprietary gear geometry, and controlled technical data are protected.
Applying Findings To Australian Aerospace Work
The value of the experiment lies in translating a statistical result into a design or operating decision. If high temperature has a strong adverse effect, engineers might revise cooler capacity, oil jet targeting, allowable temperature limits, surface finishing, or inspection intervals. If temperature is weak until combined with torque, the control strategy can focus on high-power operating windows rather than imposing a broad efficiency penalty.
For Australia, local validation can support organisations involved in defence aviation, civil operators, maintenance, repair and overhaul, and specialist manufacturing. Adelaide’s advanced manufacturing network, Brisbane’s aviation maintenance activity, and Perth’s remote-operational requirements represent different priorities for gearbox reliability and logistics. A design that reduces micropitting risk may also reduce unscheduled maintenance for aircraft working far from major overhaul centres.
Operational context matters. Aircraft supporting mining, regional transport, emergency services, or long routes across the interior may experience sustained high ambient temperatures and limited access to replacement components. A robust temperature envelope can reduce dependence on narrow operating assumptions. Findings may also support discussions with CASA-regulated maintenance organisations, although certification evidence must follow the applicable airworthiness and quality processes.
The method can be extended beyond oil temperature. Once the dominant factors are known, a second DOE could study oil flow, lubricant formulation, surface treatment, tooth microgeometry, or tolerance stack-up. Physical tests can then be calibrated against simulation, allowing engineers to explore a wider design space without manufacturing every combination. This progression supports lighter and more efficient gearboxes while keeping durability evidence visible.
Recommended Practices For A Defensible Study
- Define micropitting initiation and inspection criteria before the first run.
- Measure inlet, outlet, bulk, and relevant hardware temperatures rather than relying on one sensor.
- Include speed, torque, oil flow, surface finish, and key manufacturing variables in the screening design.
- Randomise test order and use replication or blocking to quantify experimental variation.
- Preserve raw data, oil samples, inspection images, calibration records, and analysis scripts.
- Translate significant interactions into specific limits for cooling, load, inspection, or gearbox design.
| Study condition | Likely lubrication behaviour | Main measurement priority | Engineering interpretation |
|---|---|---|---|
| Low oil temperature | Higher viscosity and potentially thicker film, with greater churning risk | Stabilisation time, flow, torque loss | Check whether efficiency penalties offset surface protection |
| Moderate operating temperature | Balanced flow, viscosity, and heat rejection | Film-related indicators and surface condition | Establish the normal design reference |
| High oil temperature | Lower viscosity and greater risk of film loss or additive stress | Mesh temperature, oil chemistry, initiation evidence | Identify thermal limits and high-risk load combinations |
| High temperature with high torque | Strong heat generation and severe contact loading | Temperature-time history and tooth mapping | Assess interaction effects relevant to high-power operation |
| Repeated thermal cycling | Changing viscosity, oxidation state, and residual surface condition | Run history and oil degradation | Separate immediate temperature effects from cumulative damage |
A well-designed DOE screening study turns oil temperature from a vague durability concern into a measurable design variable. By combining controlled thermal conditions, realistic gear loading, precise surface inspection, and statistical analysis, engineers can identify when micropitting begins and which factors accelerate it. The resulting evidence can guide safer operating limits, more efficient lubrication systems, and gearbox designs suited to demanding aircraft service.
Project teams can use these findings to shape the next phase of simulation, rig testing, and tolerance analysis through the OPTIMIZE research programme. Applying the method to representative gear hardware and documenting the results with aerospace-grade discipline will help convert early surface observations into practical gains in reliability, power density, and propulsion efficiency.