How Planet Pin Finish Shapes Journal Wear in Contaminated Oil
Planetary gearboxes operate in a demanding mechanical environment where surface texture, lubrication quality and load distribution interact continuously. The bearing journal on a planet pin may appear to be a small feature, yet its finish can influence friction, oil-film stability, debris retention and the rate at which wear develops.
In geared aircraft engines, these effects are amplified by high rotational speed, tight mass limits and fluctuating torque. A surface that performs acceptably in clean laboratory oil may behave differently when exposed to hard particles, manufacturing residue or wear debris. Understanding that difference is essential when designing compact, efficient and durable reduction gearboxes.
The OPTIMIZE research approach is relevant because it treats gearbox performance as a connected design problem. Geometry, tolerances, lubrication, manufacturing processes and physical validation need to be assessed together rather than as isolated variables. The result is a more reliable basis for selecting a planet pin finish and predicting bearing life in service.
Why Surface Finish Matters At The Journal
A planet pin journal supports the inner race or bushing associated with a planetary bearing arrangement. Its surface contains microscopic peaks and valleys created by turning, grinding, honing or polishing. These features influence the way lubricant spreads across the contact and the way the bearing surface carries load.
A relatively rough journal may cut through the lubricant film at asperity peaks, increasing metal-to-metal interaction. It can also generate additional wear particles during running-in. A highly polished surface generally reduces initial asperity contact, but an extremely smooth finish is not automatically ideal. It may retain less lubricant and can become sensitive to small particles trapped between the journal and bearing.
The most useful specification is therefore not simply “as smooth as possible”. Engineers need to consider average roughness, peak height, valley depth, surface bearing area and directional lay. Parameters such as Ra, Rz and Rpk can describe different aspects of the texture, while three-dimensional measurements reveal features that a single profilometer trace may miss.
How Contamination Changes The Contact
Contaminated oil can contain silica-like dust, machining swarf, carbon deposits, metallic fragments and degraded seal material. In an aircraft gearbox, particles may enter through maintenance activities, manufacturing residue, breather systems or component wear. Once inside the oil circuit, they can circulate through bearings and gear meshes repeatedly.
Hard particles may create indentations in the journal or bearing raceway. Softer particles can form a compacted layer that changes the effective clearance and interferes with oil distribution. A particle caught in the loaded zone can produce a local stress concentration, while a particle passing through the contact may score the journal in the direction of sliding.
Surface finish affects this process in two opposing ways. Deep valleys may hold debris away from the immediate load zone, but they can also act as reservoirs that release particles later. Sharp peaks are more likely to be flattened or torn away during operation. The preferred texture depends on bearing type, oil viscosity, operating temperature, radial load and the expected contaminant population.
Australian operating conditions make contamination control particularly practical rather than theoretical. Aircraft and rotorcraft operating near mining sites, remote communities or unsealed regional airstrips can encounter fine dust that is very different from the contaminants used in a standard clean-oil test. Maintenance teams in Alice Springs or the Pilbara may also face longer logistics chains for replacement filters and laboratory oil analysis.
Lubrication Film, Speed And Temperature
At high speed, the journal and bearing generate heat through sliding, rolling, churning and seal friction. The oil must reach the contact quickly, carry away heat and maintain sufficient viscosity under load. If the film becomes too thin, surface texture becomes a dominant factor in friction and wear.
The relationship is often assessed using a film parameter that compares lubricant-film thickness with the combined roughness of the contacting surfaces. A larger ratio generally indicates better separation, while a lower ratio means that asperity interaction is increasingly likely. Contamination can reduce the effective film margin by creating dents and scratches, even when the nominal oil viscosity remains within specification.
Temperature adds another complication. As oil warms, viscosity falls, which can reduce film thickness. A journal finish that works well during a cool ground test may experience greater wear after a long high-power flight. Compact gearbox architecture can intensify this problem because there is less oil volume and less space for heat exchangers or large sump features.
The design of oil storage and scavenging hardware is therefore closely connected to journal durability. Engineers assessing high-g manoeuvres can draw useful lessons from work on compact oil sumps, where oil location, acceleration and retention affect the quality of lubrication delivered to moving parts.
Manufacturing Route And Texture Control
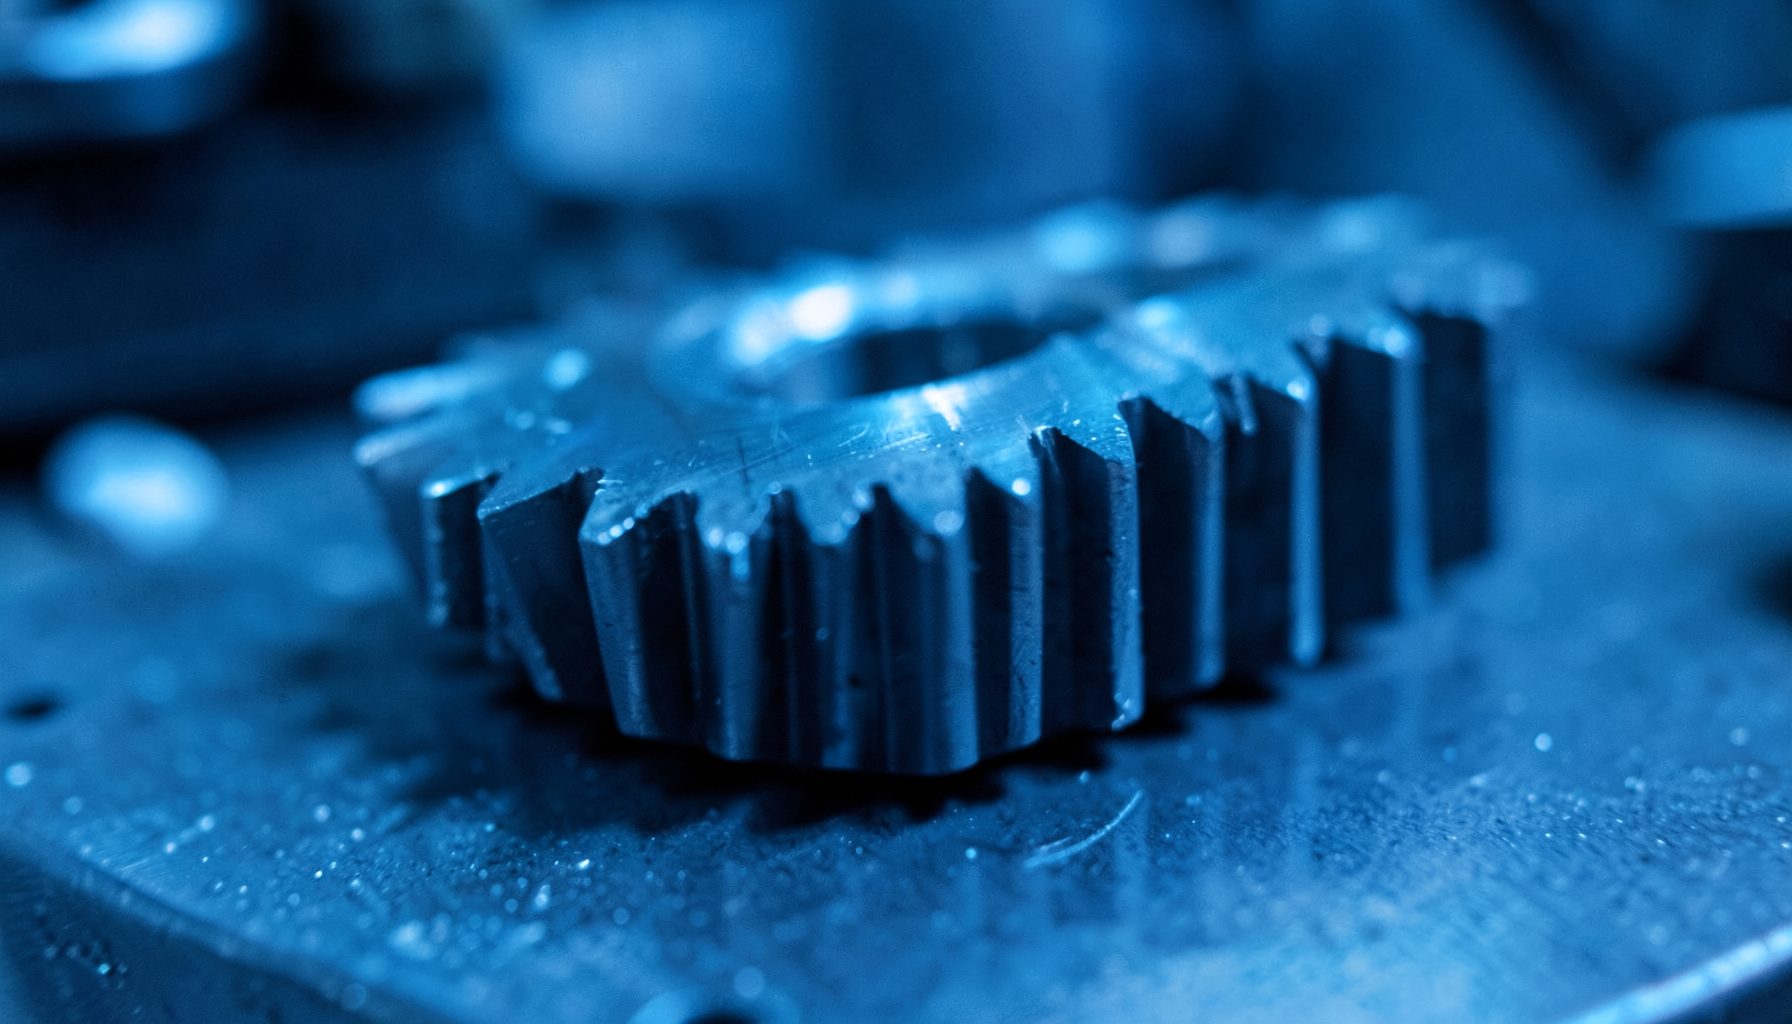
Turning is often economical and suitable for early production, but it can leave pronounced feed marks and a directional surface pattern. Grinding can produce a more controlled finish, although grinding burn, embedded abrasive and residual stresses must be monitored. Honing or superfinishing may improve the contact texture, but each added operation increases cost and introduces another opportunity for process variation.
The selected manufacturing route should reflect the actual failure mechanism. If abrasive contamination is expected, a controlled plateau finish may help reduce prominent peaks while preserving enough texture for oil retention. If fretting or adhesive wear is the concern, the balance may shift towards lower peak roughness and improved surface hardness. Coatings, nitriding or other treatments can further change friction and damage tolerance.
Inspection also needs to match the engineering objective. A single Ra limit may allow two journals with very different peak structures to pass acceptance. Production control can include stylus or optical profilometry, roundness checks, hardness verification, visual inspection for scoring and cleanliness testing after finishing.
Australian aerospace suppliers commonly work across dispersed manufacturing networks, with precision machining in areas such as Melbourne, Brisbane and Adelaide supporting operators elsewhere in the country. That geography makes process documentation and traceability important. A finish specification should be clear enough that the same journal quality can be reproduced when a part is made by a different approved supplier or after tooling changes.
Testing Wear In Representative Oil
A useful test programme should reproduce the contact pressure, speed, temperature, oil chemistry and contamination level expected in service. Test coupons, journal-and-bearing rigs or full planetary assemblies can each provide evidence, but they answer different questions. A small rig may isolate surface finish effectively, while a complete gearbox reveals interactions between load sharing, lubrication flow and housing flexibility.
Contaminant testing should identify both particle size and material hardness. A controlled quantity of aluminium, steel, silica or carbonaceous debris will create different damage patterns. The oil should be sampled during the test rather than assessed only before and after it. Particle counts, ferrous debris measurements, viscosity and oxidation indicators can show how the wear process develops.
Researchers should measure more than mass loss. Wear scar depth, journal diameter change, surface images, bearing clearance and friction torque provide a fuller picture. A journal that loses little mass but develops a deep circumferential groove may still compromise fatigue life or oil-film behaviour.
Design-of-experiments methods can reduce the number of physical tests while exposing interactions between finish, load, speed, temperature and contamination. The same statistical discipline used for gearbox mounting locations can be applied to tribology, helping engineers separate dominant variables from effects that only appear in combination.
Modelling Wear And Bearing Life
Simulation can connect measured surface data with predicted contact behaviour. Elastohydrodynamic lubrication models estimate film thickness and pressure distribution, while contact mechanics models assess how dents or scratches alter local stress. Computational fluid dynamics may help evaluate oil delivery, churning losses and the likelihood that debris reaches the bearing journal.
Wear models should be calibrated with physical evidence. Archard-type approaches can provide a starting estimate for material removal, but they may not capture three-body abrasion, particle indentation or changes in roughness over time. A model that assumes clean sliding contact can underpredict damage in contaminated oil.
Tolerance analysis is equally important. Journal diameter, bearing bore, roundness, alignment and surface texture all influence clearance and load sharing. In a hyperstatic planetary system, small geometric differences can force one planet or one bearing to carry a disproportionate share of the torque. This can make a seemingly acceptable finish fail because the local load is higher than the nominal design value.
A robust digital workflow should therefore pass manufacturing data into the simulation rather than using idealised surfaces only. Measured roughness distributions, particle exposure and thermal cycles can support a more realistic prediction of journal wear and gearbox efficiency.
Reliability, Maintenance And Australian Compliance
For Australian operators, reliability decisions are shaped by long routes, remote maintenance and the cost of aircraft downtime. A gearbox fitted to an aircraft supporting medical retrieval in northern Queensland or freight work across Western Australia may have limited access to specialised inspection equipment. Condition monitoring and clear oil-maintenance procedures can reduce the risk of a small surface defect becoming an in-service disruption.
Maintenance documentation should specify oil cleanliness targets, filter inspection intervals, sampling points and limits for journal scoring. Engineers should distinguish normal running-in debris from progressive wear. Magnetic plugs, ferrous particle sensors and laboratory analysis can complement scheduled borescope or component inspections.
Civil aviation work in Australia sits within the regulatory framework administered by CASA, with approved maintenance organisations expected to follow authorised data, documented procedures and airworthiness requirements. Defence and civil operators may apply additional internal standards. Surface finish changes should therefore be assessed through configuration control, engineering approval and traceable validation rather than introduced informally on the production floor.
Digital security and information quality also matter in a distributed engineering project. Technical teams should verify every external reference before placing it in a report or knowledge system; an unrelated online casino mirror is a useful reminder that domain names and link destinations require scrutiny. Reliable evidence should come from controlled test records, approved suppliers, recognised standards and authenticated project material.
Turning Findings Into A Gearbox Design Decision
The preferred planet pin finish should be selected from evidence that combines tribology, manufacturing capability and system performance. A decision matrix can compare candidate finishes against wear rate, friction, oil retention, contamination tolerance, production cost, inspection method and rework risk. This prevents a surface specification from being chosen solely because it has the lowest measured roughness.
The design team should also define what happens when the finish drifts outside its target. A narrow Ra tolerance may be difficult to hold across batches, while a wider but better-chosen set of parameters may deliver more consistent bearing life. Process capability studies can show whether grinding, honing or superfinishing provides the required repeatability.
Physical testing remains essential because simulation cannot capture every interaction in a contaminated planetary gearbox. Test results should feed back into geometry, oil-flow design, filtration, material treatment and inspection limits. This iterative approach supports the OPTIMIZE aim of improving efficiency, durability, weight and power density together.
Project stakeholders can use the OPTIMIZE members area to follow relevant project information and maintain a shared view of the research direction. Keeping design, manufacturing and test teams aligned is especially valuable when a small component feature such as a journal finish can affect the performance of the complete propulsion system.
Select the finish through controlled experiments, representative contamination testing and traceable inspection data. By treating journal texture as a system-level design variable, aerospace engineers can improve bearing durability, reduce avoidable wear and build geared aircraft engines that remain efficient under demanding Australian operating conditions.