Curved Teeth Spline Couplings for Fretting Mitigation at High Torque
Spline couplings form the critical torque-transmitting joints inside modern aerospace gearboxes, linking turbine sections to accessory drives and fans to reduction gearboxes. In geared turbofan and turboprop engines, these couplings operate at rotational speeds that can climb above 25,000 revolutions per minute while carrying fluctuating loads that peak during takeoff and climb-out. Engineers designing these drivetrains must manage a long list of wear mechanisms, but fretting remains one of the most stubborn. Fretting wear arises at the microscopic interface between mating splines, where tiny relative slip combines with extreme contact pressure to degrade surfaces, initiate cracks, and ultimately compromise torque capacity.
Conventional countermeasures have leaned heavily on materials engineering: harder steels, surface coatings, and lubricants fortified with extreme-pressure additives. While these approaches yield incremental improvements, they rarely target the root geometric cause of the slip. Researchers contributing to the OPTIMIZE Project have investigated a fundamentally different lever: reshaping the tooth itself. By replacing conventional straight-sided involute flanks with carefully sculpted curved profiles, designers shift the contact mechanics of the coupling so that the relative motion at the working surfaces is reduced under load. This article explores the design logic behind curved tooth spline couplings, the manufacturing realities that determine whether such profiles can be produced reliably, and the validation pathways that aerospace programs depend upon for component qualification.
Curved tooth geometry is not a single specification but a family of design choices. Variables include the radius of curvature along the flank, the location and length of the contact pattern, and the transitions at the tooth tip and root. Each of these parameters interacts with shaft deflection, housing stiffness, and lubrication behaviour, so the design process is iterative rather than prescriptive. Australian engineers collaborating with international consortia have contributed to this iterative process through finite element modelling, precision manufacturing trials, and rig testing that reflects the harsh thermal and mechanical environments encountered in service.
Fretting Behaviour in High-Torque Drivetrains
Fretting in splined joints begins with small oscillatory slip amplitudes, often measured in micrometres, that occur between mating teeth even when the overall coupling is stationary. Under high torque, the elastic stretch of the shafts and the deflection of the coupling body concentrate contact stress at specific points along the tooth flanks. As torque fluctuates during acceleration, deceleration, and steady cruise, these highly stressed regions experience alternating slip that continually disrupts the protective oxide films on the steel surfaces. Without intervention, the exposed metal beneath the oxides welds, fractures, and welds again, producing wear debris and surface roughening that accelerate the degradation cycle.
The problem is amplified in aircraft that operate across wide temperature ranges. Platforms based at RAAF Base Williamtown near Newcastle or at RAAF Base Tindal in the Northern Territory routinely see ground temperatures swing from near freezing at dawn to above forty degrees Celsius by mid-afternoon. The associated thermal expansion and contraction of shafts and housings adds differential strain to the coupling interface, driving the very micro-slip conditions that initiate fretting. Research teams at Boeing Defence Australia in Brisbane and at Monash University’s mechanical engineering laboratories have documented similar patterns when characterising engine components for both military and civil applications.
The consequences extend well beyond surface roughening. Once cracks initiate in the slip zones, they propagate under cyclic loading and can lead to tooth fracture or complete coupling failure. In a high-bypass turbofan, such a failure might ground an aircraft for unscheduled maintenance, with significant operational and financial impact. Reducing the slip amplitude at the interface therefore extends service intervals, improves power density, and contributes to the overall reliability targets that modern propulsion programmes must meet.
Curved Tooth Profile Geometry
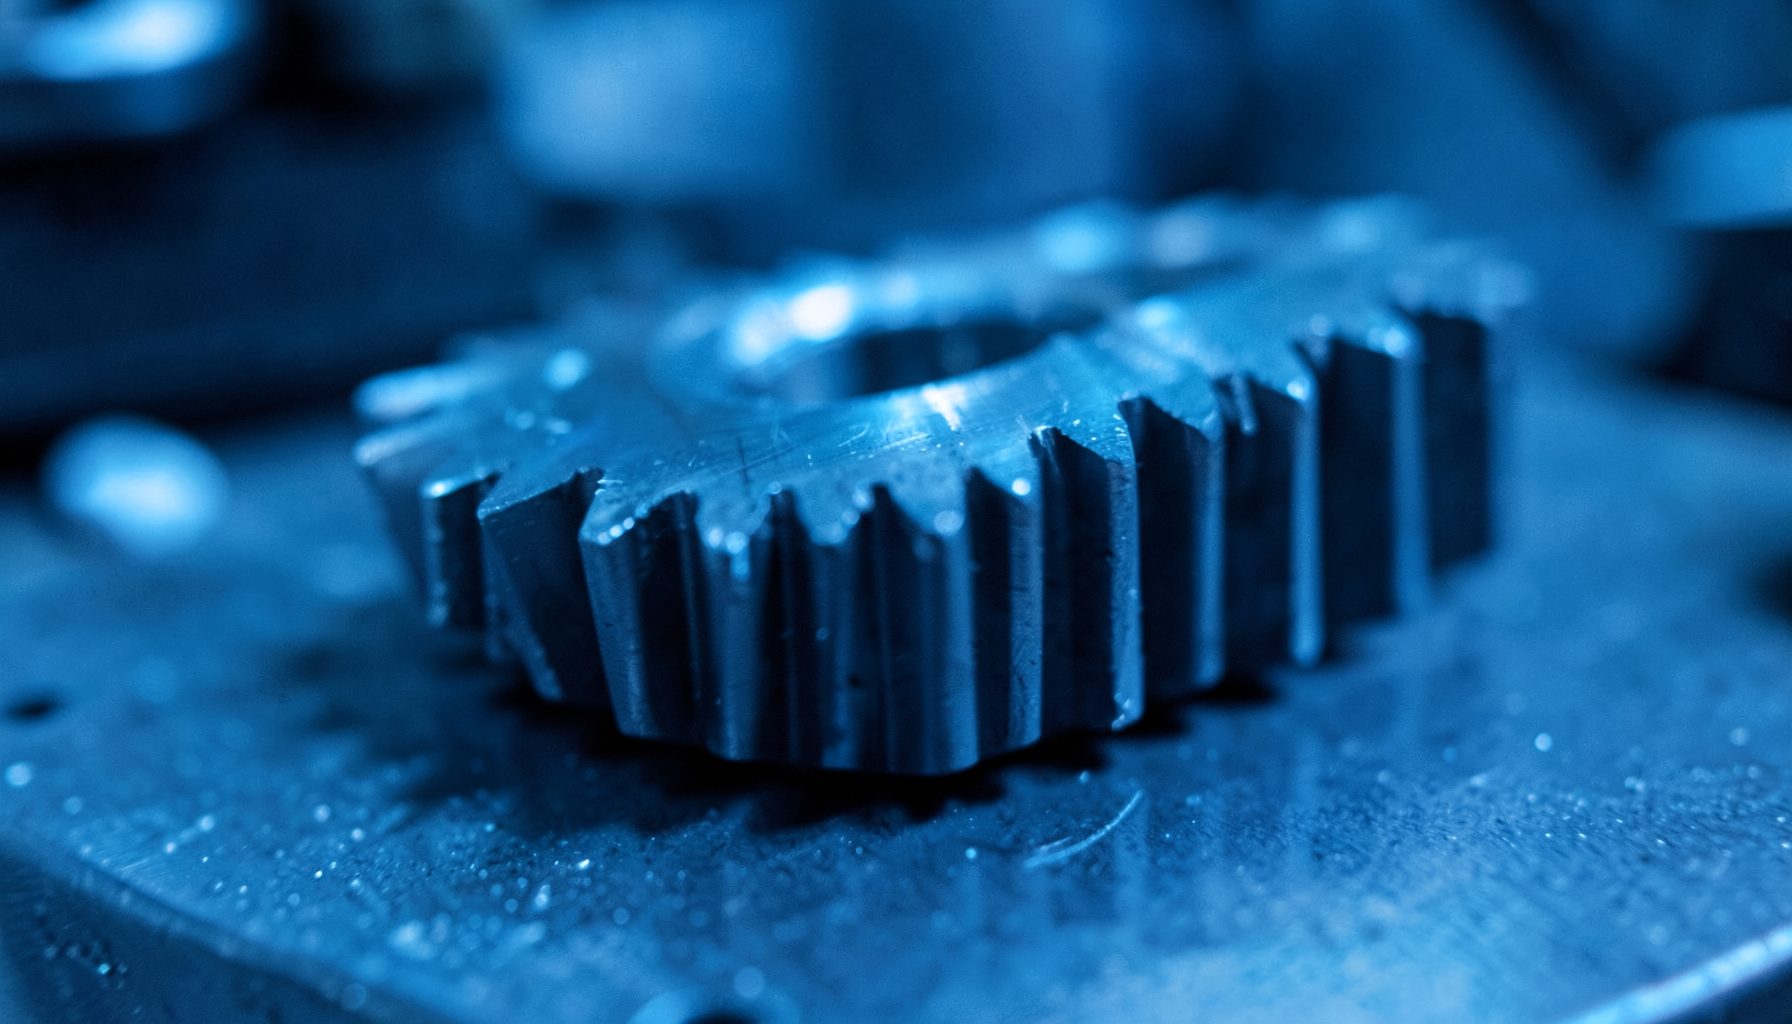
Curved tooth spline couplings replace the conventional involute flank with a deliberate arc that is tuned to the expected loading spectrum. The curvature is typically applied to the working flank, with the non-working flank often retaining a more traditional form to simplify manufacturing. When torque is applied, the curved profile causes the line of action between mating teeth to align more closely with the principal strain direction in the material, producing a contact patch that moves less under load. The result is a measurable reduction in the differential slip that drives fretting.
Designers usually begin with a baseline involute geometry, then layer modifications such as tip relief, lead crowning, and flank curvature on top. The curvature can be constant or variable along the tooth length, with variable curvature often preferred for high-torque applications. A variable radius allows the contact zone to shift gradually as load increases, avoiding the stress concentrations that occur when contact jumps abruptly from one position to another. Finite element models that capture shaft flexibility, housing constraints, and lubricant rheology guide the optimisation of these parameters, with iterations continuing until the predicted slip amplitudes fall below design thresholds. The OPTIMIZE Project team has published a tip relief study covering torque and speed conditions that complements the curved tooth approach.
Several geometric parameters govern the behaviour of a curved tooth coupling, and engineers track them closely during design refinement:
- Radius of curvature at the tooth tip, mid-flank, and root regions
- Contact pattern length and position relative to the tooth centre
- Module and pressure angle selected for the base involute
- Tip relief amount and the axial length over which it is applied
- Surface roughness specification on the working flank
Manufacturing Methods and Tolerance Control
Translating a curved tooth design into a physical component requires manufacturing processes capable of reproducing compound curves with consistent accuracy. Standard gear cutting methods such as hobbing and shaping are optimised for involute forms and struggle to produce the smooth, variable curvature demanded by advanced coupling designs. Grinding remains the benchmark for precision, but the process is slow and costly, particularly for large-diameter couplings machined from tough nickel-based superalloys.
Skiving with a profile-ground cutter has emerged as a productive alternative for coupling sizes in the medium range. The skiving cutter rotates against the workpiece and removes material in a single pass, generating a surface finish comparable to grinding while reducing cycle time. The tooling itself, however, becomes a critical variable: small deviations in the cutter profile propagate directly into the manufactured coupling, so tool wear management and in-process inspection are essential. Tolerance analysis therefore moves from a downstream check to an upstream design activity, with budgets allocated more tightly to the contact zone and more loosely to non-functional regions.
Australia hosts a concentrated base of precision aerospace manufacturers, particularly in Melbourne’s outer east aerospace corridor and around Adelaide’s Techport precinct near Osborne. These firms collaborate with research organisations including CSIRO’s manufacturing business unit and with university groups at RMIT and the University of Adelaide to qualify new processes for curved tooth components. The shared goal is to demonstrate that the required geometric tolerances can be held consistently across production batches, providing the statistical confidence that aerospace certification demands.
Surface Engineering and Lubrication Strategies
Even with an optimised geometry, spline couplings still rely on lubrication to manage heat and to protect against wear during transient operating conditions. At the speeds encountered in modern gearboxes, the lubricant film between spline teeth is often thinner than the surface roughness of the flanks, placing these components in the boundary or mixed lubrication regime. Under these conditions, the additive package in the oil, particularly extreme-pressure and anti-wear additives, interacts directly with the metal surfaces and influences both friction and fatigue life.
Surface treatments complement the geometric improvements by altering the near-surface microstructure and residual stress state. Plasma nitriding, for instance, hardens the case while introducing compressive stresses that resist crack initiation. Diamond-like carbon coatings provide a low-shear interface that can further reduce slip-driven damage. Applying these treatments uniformly across a curved flank is more demanding than for a straight involute, so process parameters such as nitriding temperature, coating throw distance, and peening intensity must be carefully calibrated to preserve the intended contact geometry.
Material selection rounds out the design package. Case-hardened steels such as AISI 9310 and vacuum-arc-remelted variants like Pyrowear 53 remain the default choices, but nitrided stainless grades and powder metallurgy materials are gaining ground in specialised applications. The pairing of pinion and coupling hardness profiles affects how contact stress distributes and how wear debris is generated. In heavy industry sectors that share similar tribological challenges, such as the mining trucks and crushing equipment operating across the Pilbara and the Bowen Basin, the lessons from aerospace lubrication research are increasingly informing maintenance practices and component life extension programmes.
Validation Programmes and Component Outcomes
Qualifying a curved tooth spline coupling requires a layered programme of analysis and testing that progresses from desktop simulation to full engine trial. The analytical phase typically begins with static structural analysis to confirm that stress levels remain within material allowables, then advances to dynamic models that capture the vibratory response of the drivetrain. Thermal modelling is integrated from the outset, since heat generation from windage and churning losses can shift material properties and lubricant behaviour over the course of a flight cycle.
Bench testing follows in purpose-built rigs that reproduce the torque, speed, and misalignment spectra of the intended application. These rigs accumulate thousands of hours of run time, with periodic inspections that track surface condition, wear debris, and temperature evolution. The data feed back into the design models, refining the predictions and justifying any design revisions. The OPTIMIZE Project runs such rigs as part of its integrated methodology, combining design-of-experiments, tolerance analysis, simulation, and physical testing to build confidence in each design iteration. Final validation occurs in engine-level trials where the coupling operates within the complete propulsion system, capturing interactions with bearings, seals, and adjacent gears that cannot be replicated on a bench rig. For Australian researchers collaborating under European programmes such as Clean Sky 2, engine trials often occur at partner facilities in Germany, France, or Italy, with subsequent teardown inspection and data analysis shared across the consortium. The methodology adopted by the project is documented on the OPTIMIZE Project website, along with project videos and updates on current research activities.
Several practical outcomes emerge from this validation work, and they inform the business case for adopting curved tooth couplings in new engine programmes:
- Extended intervals between coupling inspections reduce aircraft downtime
- Lower vibration amplitudes transmitted to the gearbox housing improve fatigue life of surrounding components
- More uniform contact stress raises the threshold for tooth bending fatigue
- Compatibility with existing lubrication systems simplifies certification and retrofit
- Potential for thinner web sections enables modest weight savings in the gearbox
Curved tooth spline couplings represent a geometric response to a wear problem that has challenged high-torque drivetrains for decades. By reshaping the working flanks of the splines, designers reduce the micro-slip that drives fretting, without relying solely on exotic materials or coatings that may introduce their own complications. The approach fits naturally within a broader engineering methodology that links design-of-experiments, tolerance analysis, simulation, and physical testing into a coherent development pathway.
For aerospace manufacturers, maintenance organisations, and research groups in Australia, the technology offers tangible operational and commercial benefits. Longer overhaul intervals, improved fuel efficiency from reduced drivetrain friction, and new opportunities in global supply chains for precision-engineered components are all part of the value proposition. The country’s existing strengths in advanced manufacturing, combined with active research collaborations in Victoria, South Australia, and Queensland, position local industry to contribute to and benefit from these developments.
Engineers and programme managers seeking deeper technical detail, project updates, or information on collaboration opportunities are encouraged to explore the resources available through the consortium. The combination of analytical rigour and practical validation that underpins the curved tooth approach offers a template for tackling other persistent tribological challenges in aerospace propulsion and beyond.