Surface Finish And Scuffing Resistance In High-Speed Gearboxes
In a geared aircraft engine, the microscopic landscape of each tooth can influence whether a transmission runs smoothly or develops a rapidly growing scuff. Surface finish affects how oil enters the contact, how asperities carry load, and how much heat remains at the sliding interface. These effects become especially important when speed, torque, temperature and limited lubricant supply push the gear mesh towards boundary lubrication.
For the OPTIMIZE Project, this subject fits within a broader effort to reduce power losses while improving durability, mass and power density. A finish that looks excellent in a laboratory measurement may perform poorly after manufacturing variation, thermal distortion or an interrupted oil jet changes the real contact conditions. Understanding the link between surface texture and scuffing resistance therefore requires surface metrology, simulation, tolerance analysis and physical testing together.
Why Boundary Lubrication Raises The Stakes
A gear tooth normally relies on an elastohydrodynamic lubrication film. Pressure and viscosity create a thin film that separates much of the contacting material, allowing the teeth to transmit load with limited direct metal contact. The lambda ratio, calculated by comparing film thickness with the combined surface roughness of the two bodies, is a useful guide to this regime.
At high speed, the oil film can become thinner because of temperature rise, starvation or changes in viscosity. During starts, stops, rapid torque changes and oil-supply disturbances, the contact may move into mixed or boundary lubrication. In that state, the highest asperities interact directly. Friction increases, heat concentrates in small areas and adhesive junctions can form between opposing surfaces.
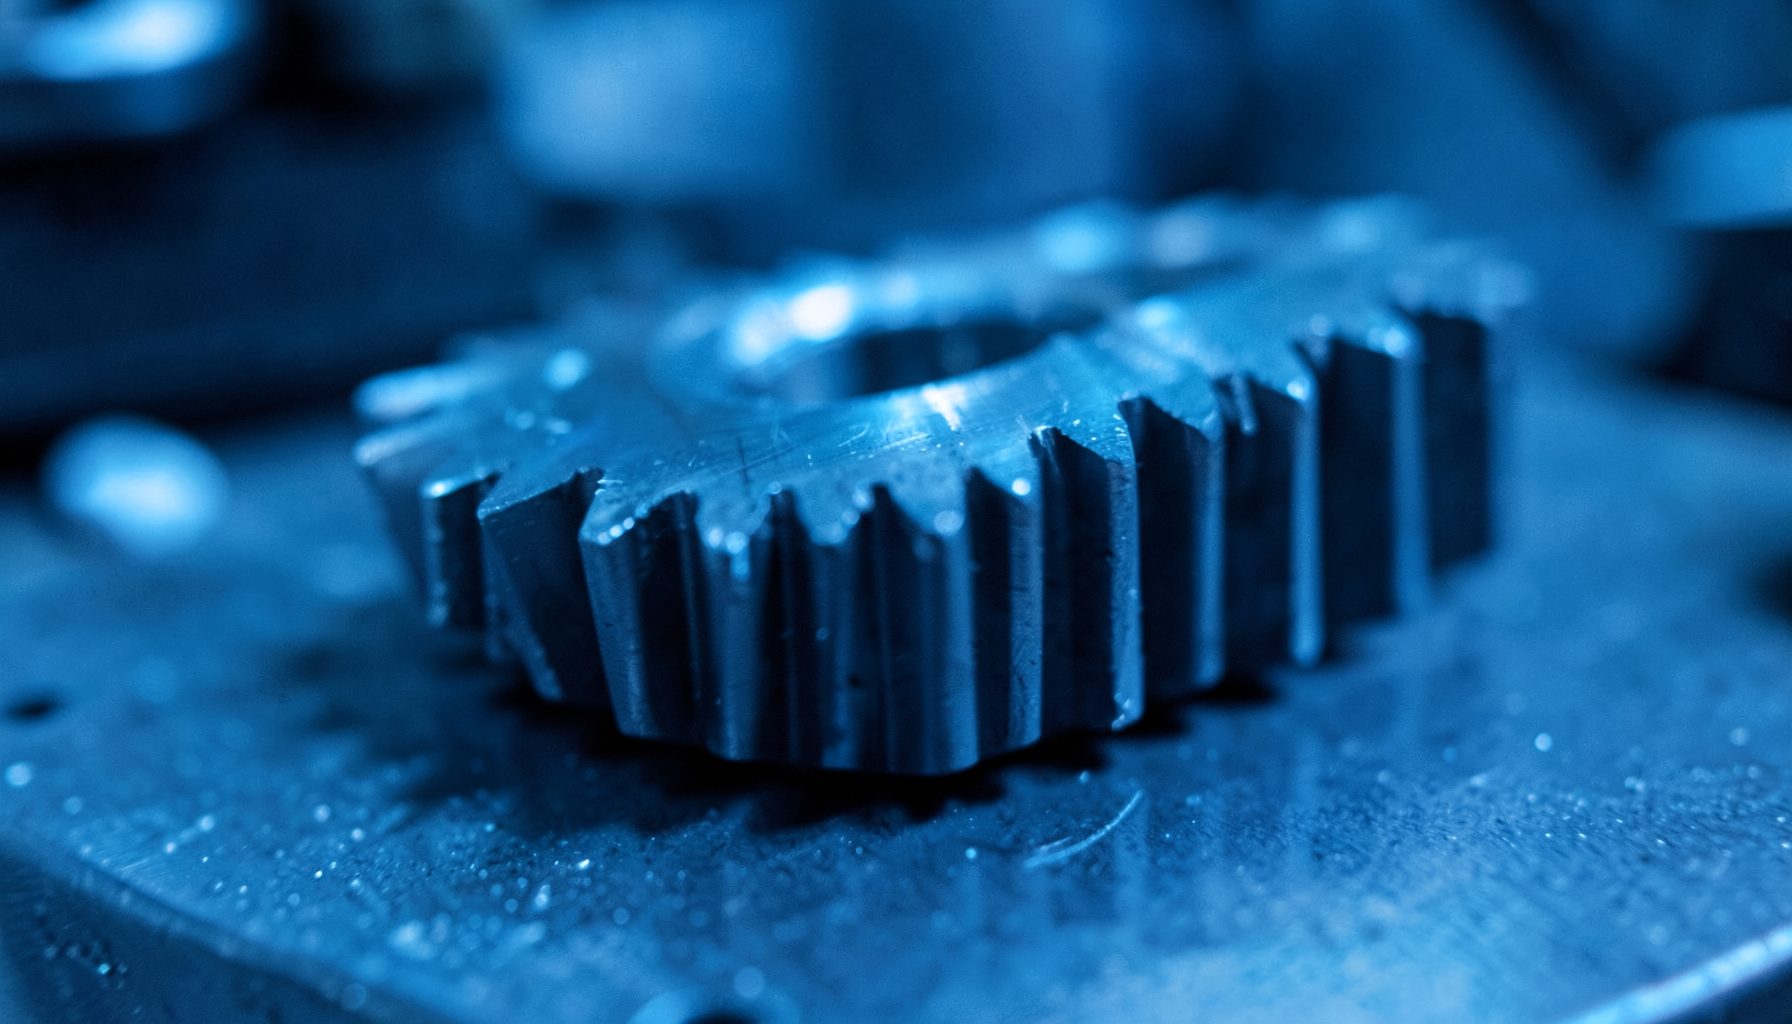
Scuffing is a severe form of this process. Local welding and tearing remove material from the tooth flanks, producing rough streaks in the sliding direction. The damage can then increase friction and generate more heat, creating a feedback loop. A carefully selected finish cannot compensate for inadequate oil flow or excessive load, yet it can provide a valuable margin before that loop begins.
What Surface Texture Does Inside The Mesh
Average roughness, often reported as Ra, is only one part of the picture. Rq describes the root-mean-square height variation, while parameters such as Rsk and Rku indicate whether the texture is dominated by valleys, peaks or unusually sharp features. Rz gives information about the height of prominent irregularities. Two gear flanks with the same Ra can therefore have very different scuffing behaviour.
Sharp peaks are particularly undesirable because they create high local pressure and penetrate a thin lubricant film. A controlled plateau finish reduces the tallest asperities, lowering the chance of direct interference during sliding. However, removing every valley can reduce the surface’s ability to retain oil. A useful texture usually balances low peak height with enough connected valleys to support lubricant replenishment.
Grinding direction matters as well. If lay marks run across the direction of sliding, they may assist lubricant entrainment under some conditions. If they create continuous ridges aligned unfavourably with sliding, they can increase friction and act as initiation sites for distress. Honing, isotropic superfinishing and carefully controlled grinding can alter both the amplitude and directionality of these features.
Measuring Finish Beyond A Single Ra Value
Aerospace gearbox development needs repeatable measurements that relate to actual contact performance. Stylus instruments remain useful for profile readings, while optical methods can capture areal texture without touching a delicate finished flank. Measurements should cover the active tooth region, including zones near the tip, pitch line and root, because finishing quality may vary across the flank.
The surface should be assessed after the full manufacturing route, rather than immediately after a nominal finishing operation. Heat treatment, shot peening, grinding burn, superfinishing and cleaning can all change the texture. A result measured before assembly may not represent the condition after handling, run-in or exposure to the selected oil and additives.
Functional testing then links metrology to engineering decisions. A twin-disc rig or gear test machine can apply representative sliding speed, contact stress, temperature and lubricant flow. Scuffing load-stage tests help establish a failure threshold, while endurance tests reveal whether a finish supports stable operation over many cycles. Surface microscopy after testing can distinguish mild polishing from adhesive transfer and progressive scoring.
Matching Finishing Processes To Gear Materials
Grinding is common for hardened aerospace gears because it can deliver accurate geometry and a controlled profile. Its risks include grinding burns, tensile residual stress and directional marks that remain active under sliding. Process parameters, dressing condition and coolant delivery need close control, especially when a high-speed reduction gearbox uses small pinions with concentrated contact stresses.
Honing and isotropic superfinishing can reduce asperity height after grinding. Chemical-mechanical processes may produce a smoother, more isotropic surface with lower friction, although excessive treatment can alter tooth geometry or remove useful oil-retaining features. The right target depends on material hardness, case depth, tooth size, lubricant chemistry and the expected duty cycle.
Coatings introduce another variable. Diamond-like carbon, tungsten carbide carbon and other low-friction systems can reduce adhesion when correctly applied, but coating thickness, adhesion, surface preparation and edge coverage must be controlled. A coating on an inadequately finished substrate may reproduce underlying defects or fail under high Hertzian stress. For Australian manufacturers supplying specialist aerospace work, this makes traceable process control and qualified subcontractors commercially important, particularly when production volumes are too small to support repeated trial-and-error.
Lubricant Supply And Surface Finish Work Together
A smooth flank cannot protect a mesh that is intermittently starved of oil. Jet position, flow rate, pressure, droplet breakup and churning losses determine how much lubricant actually reaches the active contact. This is why research into oil jet pulsation is relevant to surface durability: a fluctuating supply can repeatedly remove the film margin that a carefully finished tooth was designed to preserve.
Oil additives also interact with the surface. Extreme-pressure and antiwear chemistry can create protective films during boundary operation, but their effectiveness depends on temperature, reaction time and material compatibility. A finish that works well with one ester or synthetic formulation may behave differently with another. Testing should therefore use the intended lubricant, including its additive package, rather than relying on a generic oil.
High-speed operation adds thermal complexity. Windage and churning heat raise bulk oil temperature, while flash temperature at asperity contacts may be much higher. In Brisbane or Darwin operating conditions, ambient heat can reduce the available viscosity margin during ground operation and climb. The gearbox design needs enough cooling and oil delivery capacity to ensure the surface specification remains effective across the complete thermal envelope.
Load Sharing Changes The Scuffing Risk
Planetary gearboxes have several meshes sharing torque, but manufacturing variation and structural flexibility can prevent perfect load distribution. A planet that carries more than its intended share may experience higher contact stress and greater sliding heat. Surface finish becomes one part of a larger system involving alignment, bearing clearance, housing stiffness and tooth modifications.
The number of planets also affects load capacity, packaging and power density. Work on planet gear selection shows why a nominally efficient arrangement still needs careful assessment of load sharing and dynamic behaviour. More planets can increase torque capacity within a compact envelope, yet they can amplify sensitivity to assembly errors and circumferential spacing.
Flexible gear bodies and joints create further variation. A dovetail or other attachment can change local stiffness and alter how vibration reaches the tooth contact. The relationship between gear body joints and dynamic response matters because fluctuating torque can repeatedly move the mesh into a higher-friction state. A finish that passes a steady-load test may have less margin under torsional oscillation.
Designing A Practical Surface Specification
A useful specification should state more than “superfinished” or provide a single Ra limit. It can define roughness parameters, measurement cut-off, evaluation length, lay direction, waviness limits, inspection locations and acceptable peak features. It should also identify the post-treatment condition, because polishing, coating and cleaning can change the final result.
The specification needs to be tied to the duty cycle. A lightly loaded accessory gearbox may tolerate a different texture from a compact reduction stage transmitting high power at high pinion speed. Designers should consider sliding velocity, contact ratio, peak torque, transient events, oil temperature, lubricant viscosity and the acceptable scuffing risk. Simulation can map these variables, while design-of-experiments methods reveal which factors have the strongest influence.
Tolerance analysis is essential when the target finish is close to the process capability limit. Variation in case hardness, tooth lead, profile error, alignment and roughness can combine unfavourably. Instead of asking whether one ideal gear survives, engineers can estimate the performance distribution across a production batch. This approach supports realistic limits and helps avoid an expensive specification that delivers little additional reliability.
Validating Performance From Rig To Aircraft
Validation should progress from controlled coupons and twin-disc tests to representative gears, then to a complete gearbox. Early testing isolates the influence of texture and lubricant. Gear tests introduce tooth geometry, rolling-sliding contact, dynamic load and realistic heat generation. Full-system tests reveal effects from bearings, shafts, housing deformation, oil aeration and control-system behaviour.
Instrumentation can include torque, speed, oil pressure, inlet and outlet temperature, vibration and debris monitoring. Endoscopic inspection and microscopy help identify the first signs of polishing, micropitting or adhesive transfer. Scuffing resistance should be judged alongside efficiency and wear, since a finish that reduces friction but accelerates micropitting may not provide a sound aerospace solution.
This staged method suits Australia’s specialised aerospace market, where Adelaide’s defence and manufacturing capability, Melbourne’s engineering networks and local university laboratories can support collaborative qualification work. Components may pass through several suppliers before reaching an integrator, so digital records for surface measurements, heat treatment and inspection are valuable. CASA compliance, customer audits and export requirements also reward a clear evidence trail rather than informal process knowledge.
A gearbox intended for service near Perth, Townsville or remote Australian airfields may face different maintenance logistics from a system operated in a major European hub. Robust scuffing margins reduce the chance that a minor oil-system deviation becomes a grounded aircraft or an urgent freight movement. That practical value gives surface engineering a direct connection to fleet availability.
Surface finish is therefore a design variable, not a cosmetic afterthought. The best result comes from combining texture control with reliable oil delivery, suitable chemistry, accurate load sharing and validation under representative transients. Apply the OPTIMIZE Project’s engineering approach by connecting surface metrology, simulation, tolerance studies and physical testing into one development loop for efficient, durable high-speed gearboxes.